NOTICE
We use cookies to improve the user experience and analyze its performance.
Choosing an Aluminum Die Cast Mold supplier is a production decision, not merely a purchasing task. The right partner influences cycle time, part accuracy, tool life, maintenance cost, and delivery stability. A polished sample cannot hide weak engineering forever.
Grand View Research reported that the global die casting market was valued at approximately USD 87 billion in 2023. It also projects continued growth through 2030, driven by automotive lightweighting and electric-vehicle production. The U.S. Department of Energy notes that reducing vehicle weight can improve fuel economy by roughly 6% to 8% for every 10% reduction. These trends increase demand for reliable aluminum tooling.
According to Dan Twarog, former president of the North American Die Casting Association, “A die is not just a tool; it is the foundation of consistent die-casting production.” His point deserves attention. A supplier should understand alloy behavior, thermal balance, gating design, venting, cooling channels, and realistic maintenance intervals.
Ask for measurable evidence. Review mold-flow analysis, steel certificates, dimensional inspection records, and previous projects with similar wall thicknesses. Examine the supplier’s response to porosity, soldering, flash, and premature cracking. Factory visits can reveal more than attractive brochures.
Cost still matters. However, the lowest quotation may create expensive downtime later. Sometimes, it does.
A strong supplier also communicates uncomfortable facts. They may challenge an unrealistic tolerance or recommend a design change. That is valuable experience, although it can feel inconvenient. Before signing, compare engineering capability, testing discipline, spare-part support, and total ownership cost—not only the first invoice.
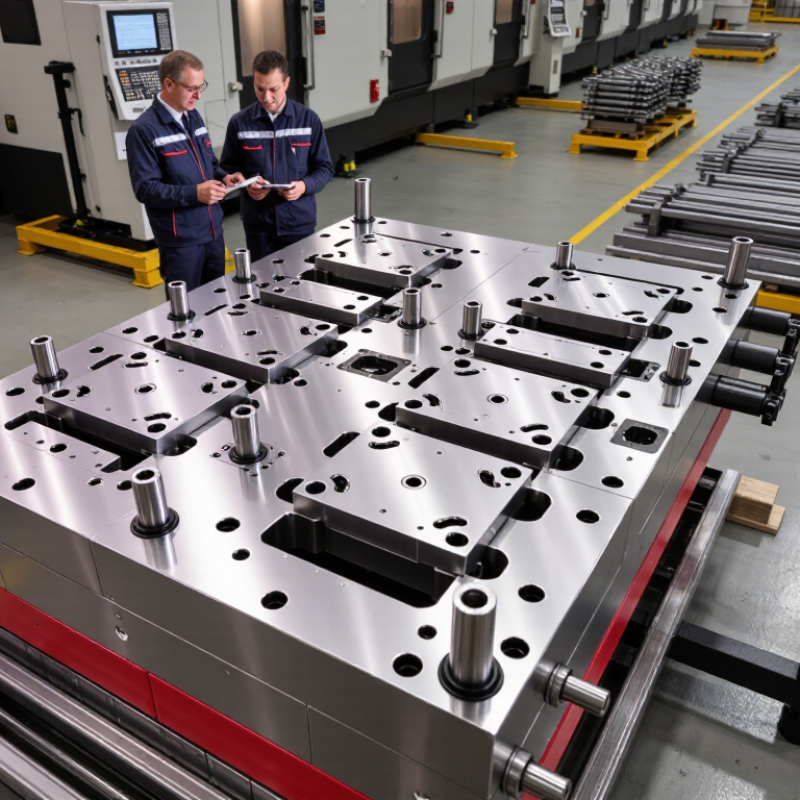
Before contacting a supplier, document the part’s alloy, dimensions, wall thickness, and expected production volume. Include the drawing revision. Small changes can affect cavity design, cooling channels, and ejector placement.
State critical tolerances clearly. Separate functional surfaces from cosmetic surfaces. Specify draft angles, parting lines, threaded features, and acceptable flash. A supplier cannot price a reliable mold from a vague three-dimensional file alone. Mention the intended casting machine, shot capacity, and available clamping force. These details help engineers check mold compatibility before cutting steel.
Think beyond the first sample. Estimate annual output, cycle time, maintenance access, and the required mold life. Ask whether replaceable inserts are practical for high-wear areas. Also define inspection needs, including dimensional reports, leak testing, or sample approval criteria. Keep the requirement list measurable.
Our early projects sometimes focused too heavily on tooling cost. That choice created longer maintenance delays later. A cheaper design is not always economical. Cooling performance, steel selection, and repair access deserve equal attention. Request a design review with filling analysis and likely defect risks. The result may expose an inconvenient truth: the part design itself needs adjustment. That conversation is useful. It shows whether the supplier can explain trade-offs with evidence, not promises.
A supplier’s experience should match your part’s complexity, alloy, and expected production volume. Ask how many comparable molds they have completed, not just how long they have operated. Review sample drawings, trial records, and documented corrections from previous projects. This reveals practical judgment under pressure. It also exposes weak process control.
Equipment shows whether the supplier can protect your design intent. Look for modern CNC machining, EDM, wire cutting, and coordinate measuring equipment. Reliable suppliers should verify cavity dimensions, parting lines, ejector locations, and cooling channels. Mold-flow analysis can identify filling problems before steel is cut. During trials, request measured results for flash, porosity, shrinkage, and cycle stability. A supplier with technical depth explains causes clearly, rather than blaming the machine or operator. Their records should connect material certificates, machining data, inspection reports, and revision history. Small gaps matter.
Tips: Ask to inspect the workshop, even through a live video call. Request a trial plan with acceptance criteria. Confirm who approves design changes. Compare actual tolerances with promised tolerances. Do not accept attractive pricing without checking maintenance support and spare-part planning. One honest warning is valuable: no supplier is perfect, and early assumptions can be wrong. Leave room for a second design review.
Choosing an aluminum die cast mold supplier starts with steel, not a polished brochure. The mold should use certified hot-work tool steel, such as H13 or an equivalent grade. Ask for mill certificates, heat-treatment records, and hardness results. These documents confirm composition and thermal stability. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 estimates global aluminum production reached about 72 million metric tons in 2024. Such volume increases pressure on mold life and repeatability. Small material shortcuts can create large production losses.
Precision must be measurable. Request a drawing with GD&T, datum references, cooling-channel locations, and target surface roughness. A coordinate measuring machine should verify critical dimensions after machining. The NADCA Product Specification Standards provide recognized guidance for die casting dimensions, machining allowances, and process control. Do not accept “high precision” without inspection records. Ask for actual capability data, including Cp and Cpk, for critical features. One sample is not evidence. It is only a beginning.
Quality control should follow the mold from design to trial shots. Require design reviews, steel traceability, electrode inspection, vent checks, and documented trial corrections. A supplier using SPC can identify drift before flash or porosity appears. ISO 9001 certification supports controlled procedures, but it does not guarantee excellent molds. That distinction matters. Even a careful checklist can miss poor cooling balance or unstable ejection. Review sample reports, question unusual tolerances, and inspect the supplier’s measurement equipment calibration. Candor is valuable; no mold is perfect.
Choosing an aluminum die cast mold supplier requires more than comparing hourly rates. Start with prototyping capability. Ask whether the supplier can provide flow analysis, rapid tooling, sample inspection, and documented design changes. A prototype should reveal porosity, draft problems, parting-line risks, and machining allowances before production tooling begins. Small details matter. The U.S. Department of Energy reports that aluminum components can reduce vehicle weight by roughly 40–50% versus steel components. That makes accurate geometry and repeatable filling especially important in lightweight applications. A supplier that skips simulation may offer a lower price, but the first trial can become expensive rework.
Production capacity must match your real demand, not an optimistic forecast. Review machine tonnage, alloy control, tool-life planning, and inspection equipment. NADCA’s Product Specification Standards emphasize process control, dimensional verification, and casting-quality requirements. Request evidence, such as capability studies, gauge records, and previous production samples. Pricing should separate mold design, steel, machining, trials, maintenance, and engineering changes. The cheapest quotation is often incomplete. Sometimes, an apparently premium mold reduces unit cost across a long production run.
Delivery promises need measurable milestones. Compare design approval, steel ordering, machining, first-shot trials, correction cycles, and final acceptance. The World Bank’s 2023 Logistics Performance Index shows that international shipments still face differences in customs efficiency, infrastructure, and timeliness. Therefore, ask for a realistic shipping plan and contingency options. Build a buffer. I have seen schedules fail because one revised drawing was treated as a minor change. A reliable supplier records every revision, confirms responsibility, and reports delays before they affect assembly.
| Evaluation Dimension | Prototype-Focused Supplier | Production-Focused Supplier | Hybrid Supplier | What to Verify Before Ordering |
|---|---|---|---|---|
| Best Fit | Design validation, fit checks, and early functional samples | Stable demand, repeat orders, and high annual production volumes | Projects that require a smooth transition from sampling to mass production | Whether the supplier has equipment and quality controls suitable for the complete project life cycle |
| Typical Order Quantity | 1–500 parts for initial evaluation | Usually 10,000+ parts per year, depending on part size and machine capacity | Approximately 100–100,000+ parts, subject to tooling and production planning | Minimum order quantity, annual capacity, and reserved production slots |
| Prototype Method | CNC machining, 3D-printed patterns, soft tooling, or limited die casting | Production-grade steel die with validated casting parameters | Rapid prototype route followed by production die optimization | Whether prototype geometry, alloy, wall thickness, and finishing requirements represent the final part |
| Tooling Lead Time | About 1–4 weeks for soft or simplified tooling | About 6–12 weeks for a new production die, depending on complexity | About 3–8 weeks when prototype learning is incorporated into the final die design | Detailed schedule covering design review, machining, trial shots, corrections, and approval |
| Sample Delivery | Approximately 2–6 weeks after design approval | Approximately 8–16 weeks for first production samples | Approximately 4–10 weeks, depending on the prototype route and tooling status | Whether delivery time includes inspection, surface treatment, packaging, and freight |
| Indicative Tooling Cost | Approximately USD 500–10,000 for simplified or low-life tooling | Approximately USD 8,000–80,000+ for complex multi-slide production dies | Approximately USD 3,000–50,000, depending on cavity count, part size, and die life | Steel grade, cavity count, sliders, inserts, expected die life, maintenance, and ownership terms |
| Part Price at Low Volume | Usually higher because tooling and setup costs are spread over fewer parts | Often less competitive below the supplier’s efficient batch size | Moderate; may offer both machined and die-cast options | Fully loaded unit price, including setup, scrap allowance, inspection, finishing, and packaging |
| Part Price at High Volume | May increase if the supplier lacks automated cells or sufficient machine capacity | Generally strongest due to automated casting, trimming, inspection, and repeatability | Competitive when the same process and tooling can be scaled successfully | Quoted price breaks, annual volume assumptions, material surcharge formula, and capacity commitment |
| Dimensional Capability | CNC prototypes can achieve tight dimensions, but they may not represent die-cast variation | Common as-cast tolerances are often around ±0.1–0.3 mm for selected dimensions; tighter features may require machining | Can combine die casting with secondary machining for critical datums and holes | Supplier’s tolerance standard, measurement method, datum scheme, and capability study for critical features |
| Surface Finish | Machined surfaces can be smooth; prototype cast surfaces may show draft, ejector, and parting marks | Typical as-cast surfaces may be approximately Ra 3.2–12.5 μm, depending on process and area | Can coordinate blasting, tumbling, machining, powder coating, anodizing, or painting | Approved surface samples, roughness limits, cosmetic zones, and treatment subcontractor controls |
| Quality Documentation | Basic inspection report and sample feedback are commonly available | 通常 includes control plans, process records, traceability, dimensional reports, and corrective-action procedures | Documentation can cover both prototype learning and production control | Inspection standard, material certificate, test requirements, traceability, and nonconformance process |
| Production Equipment | CNC equipment, small die-casting machines, and flexible manual operations | Die-casting machines, trimming presses, automated cells, heat-treatment capability, and dedicated inspection equipment | A mix of prototype machining, die casting, secondary machining, and finishing resources | Machine clamping force, shot capacity, furnace controls, automation level, and backup equipment |
| Delivery Reliability | Flexible for small quantities, but schedules may depend on shared equipment | Usually stronger for scheduled repeat orders with forecasted demand | Good when one project manager controls tooling, production, and logistics | On-time delivery history, capacity plan, holiday schedule, logistics terms, and contingency plan |
| Recommended Selection Priority | Speed, design feedback, flexibility, and low initial commitment | Repeatability, total cost per part, capacity, process control, and long-term supply security | Single-source coordination, scalable tooling, and balanced development risk | Choose according to volume, launch date, part complexity, required tolerance, and total landed cost |
Note: Cost, lead-time, tolerance, and surface-finish figures are typical industry planning ranges for aluminum die-casting projects. Actual results depend on part size, alloy, wall thickness, draft angle, cavity design, order volume, inspection requirements, and shipping location.
Communication often reveals a mold supplier’s real working habits. Ask for a clear project schedule, drawing review process, and response-time standard. During my supplier evaluations, reliable teams shared marked-up drawings, inspection photos, and risk notes before production. Vague replies created more delays than difficult tooling problems. McKinsey’s 2020 global supply-chain survey found that 93% of leaders had taken resilience-building actions. Supplier communication belongs in that plan. It affects design changes, trial schedules, and emergency decisions.
Tips: Request one technical contact and one escalation contact. Ask for weekly updates with photographs. Check whether meeting notes identify owners and deadlines. Review after-sales support carefully. A dependable supplier should provide mold maintenance guidance, spare-part recommendations, and troubleshooting records after delivery. The ISO Survey 2023 reported more than one million ISO 9001 certificates worldwide, but certification alone proves little about responsiveness. Ask for anonymized service records and typical corrective-action times. A polished audit file can still hide weak follow-up.
Reliability needs evidence across several projects. Examine on-time trial results, cavity-life records, repair history, and customer references from similar aluminum alloys. I would also test a small engineering change before awarding a full program. It may feel inefficient. Yet this exposes communication gaps early. Keep the scorecard practical: technical accuracy, reply speed, after-sales ownership, documentation quality, and recovery performance when something goes wrong.